Global leader in silver-ion technology and high-performance hygienic PVC flooring solutions for medical, commercial, and residential spaces.
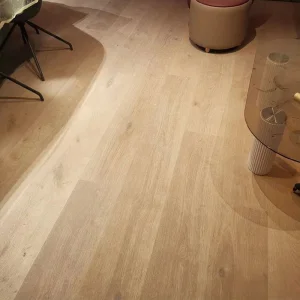
In the wake of heightened global awareness regarding hygiene and safety, the Anti Bacterial Flooring industry has evolved from a niche medical requirement to a fundamental standard in commercial and residential architecture. Today, the global market for hygienic flooring solutions is expanding at a CAGR of 6.5%, driven by the relentless pursuit of environments that actively inhibit the growth of harmful pathogens such as Staphylococcus aureus and E. coli.
From the bustling healthcare corridors in North America to the high-tech laboratories of Europe, architects and facility managers are no longer compromising. As a leading Anti Bacterial Flooring Manufacturer & Factory, we understand that "clean" is no longer just a visual metric—it is a chemical and biological imperative built directly into the surface of our LVT and LVP products.
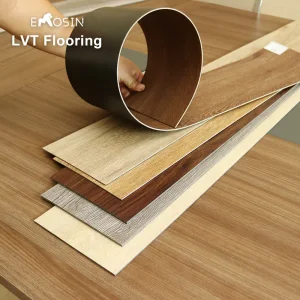
Bacterial Reduction Rate
Countries Exported To
Commercial Durability
Formaldehyde Emissions
The industry is moving beyond passive surfaces. Modern Anti Bacterial Flooring now incorporates silver-ion technology and photocatalytic coatings that work 24/7 to decompose organic matter.
As a specialized factory, we stay ahead of these trends by investing 15% of our annual revenue into R&D, ensuring our clients receive the most advanced flooring planks available in the market.
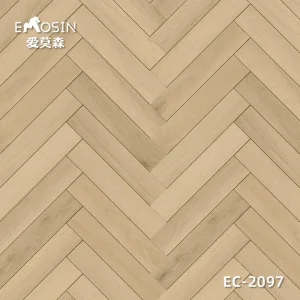
Global sourcing managers look for three key pillars: Compliance, Consistency, and Cost-efficiency. Whether you are a developer in Dubai or a contractor in Berlin, our factory provides localized solutions for diverse scenarios.
Sterile environments requiring seamless, easy-to-clean surfaces that resist chemicals and moisture.
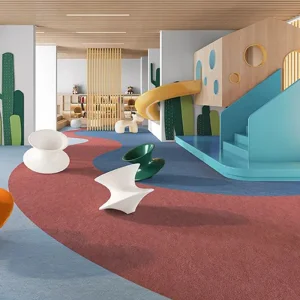
Heavy-duty, slip-resistant flooring for classrooms where kids' health and safety are paramount.
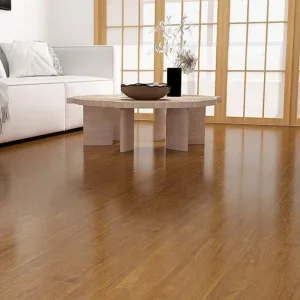
Sophisticated LVT designs that offer "home-like" warmth with commercial-grade antimicrobial protection.
Homeowners seeking "Pet-Friendly" and "Allergy-Safe" flooring that is 100% waterproof and durable.
Choosing a Chinese Anti Bacterial Flooring Factory offers unparalleled strategic advantages in today’s competitive landscape. We combine the world's most robust supply chain with cutting-edge manufacturing precision.
1. Unbeatable Supply Chain: Being located in the industrial heart of Guangzhou, we have immediate access to high-quality virgin PVC and advanced antimicrobial additives, reducing lead times and costs.
2. OEM/ODM Capability: We don't just sell products; we create solutions. From customized wear layer thicknesses to unique branding on packaging, we empower global brands to scale rapidly.
3. Rigorous Quality Control: Every batch of flooring undergoes a battery of tests, including VOC emission tests, anti-slip ratings, and 48-hour moisture immersion tests.
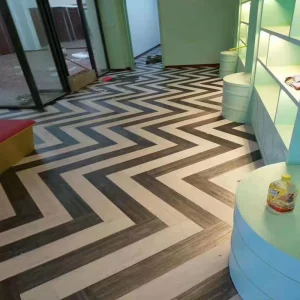
Welcome to Guangzhou DCTan Door Co., Ltd.—your trusted partner in high-quality, durable, and stylish solutions. Based in Guangzhou, China, a city renowned for its excellence in building materials and manufacturing, we are a leading manufacturer specializing in the design, production, and supply of a wide range of surfaces and architectural elements for residential, commercial, and industrial use.
With state-of-the-art production equipment, a dedicated team of skilled professionals, and a robust technical foundation, DCTan has positioned itself at the forefront of the building material industry. We produce a diverse range of products including entry solutions, interior finishes, and customized solutions tailored to meet the specific needs of our clients. Whether you require sophisticated, high-security solutions or stylish designs that enhance aesthetics, we provide products made from the finest materials, such as aluminum alloy, solid wood, vinyl, and steel.
At DCTan, quality is our top priority. All our products are manufactured in strict adherence to international standards and undergo rigorous testing to ensure they meet the highest levels of safety, performance, and durability. Our commitment to quality is reflected in our authoritative certifications:
These certifications are a testament to our commitment to safety, environmental responsibility, and compliance with global market standards.
We are proud to offer both OEM and ODM services, providing tailor-made solutions for Residential Projects, Commercial Buildings, Hospitality, and Industrial Spaces. While we are based in China, our products reach customers worldwide across Europe, North America, Asia, Africa, and Australia.
The science behind Anti Bacterial Flooring involves the integration of active agents into the top wear layer of the vinyl. Unlike topical sprays that dissipate over time, our factory utilizes a molecular bonding process where silver ions (Ag+) are suspended within the transparent wear layer. When bacteria land on the surface, these ions puncture the cell walls of the microorganism, effectively halting their metabolic process and preventing reproduction. This technology is crucial in high-traffic commercial zones where surface contamination is a constant risk.
In the industrial sector, flooring must withstand more than just microbes. It must endure heavy rolling loads, abrasive cleaning agents, and constant UV exposure. Our Commercial Vinyl Planks are engineered with a cross-linked UV coating that enhances stain resistance while maintaining its antimicrobial efficacy for decades. This makes it an ideal choice for hospital operating theaters, dental clinics, and food preparation areas where ISO standards for cleanliness are non-negotiable.
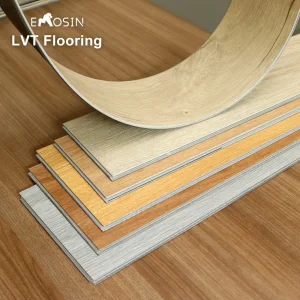
Furthermore, as a Top Best Anti Bacterial Flooring Manufacturer, we prioritize the environmental impact of our production. All our raw materials are sourced from sustainable streams, and our manufacturing process is designed to minimize waste. By choosing LVT (Luxury Vinyl Tile) over traditional materials like hardwood or carpet, users benefit from a product that doesn't trap dust mites or allergens, contributing to significantly better Indoor Air Quality (IAQ).
The global demand for these products is particularly high in regions like Western Europe and North America, where building codes are becoming increasingly stringent regarding public health safety. We have responded to this demand by scaling our production capacity and obtaining global certifications that ensure our flooring meets the fire safety, slip resistance, and emission standards required for modern infrastructure projects.
For developers and distributors, the key advantage of partnering with our China Factory lies in our ability to provide premium tech-integrated flooring at a price point that makes large-scale projects viable. We offer complete transparency in our testing protocols, providing COA (Certificate of Analysis) for every shipment. This level of professionalism has cemented our status as a preferred supplier for international hotel chains and government-funded healthcare initiatives across the globe.
 DCTan Door